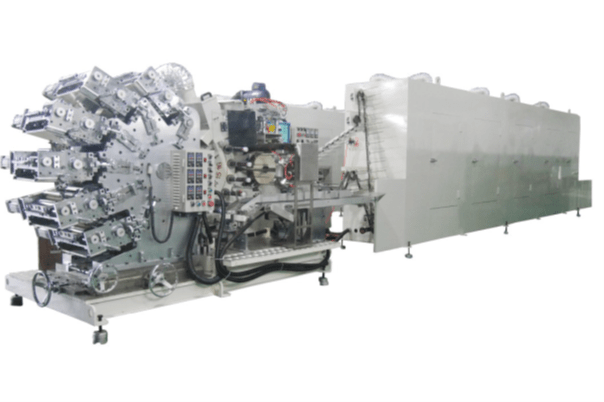
Screen printing is increasingly popular for coextruded PE cosmetic tubes, with customers often requesting designs in as many as six colours. As a result, major PE tube manufacturers are investing in fully automatic UV screen-printing machines equipped with UV varnish and five or six colour stations. Some manufacturers that previously relied solely on dry-offset printing have added screen printing to their capabilities, while those with existing facilities have installed additional machines to multiply production capacity. Most of these automatic machines have been supplied by reputable Chinese manufacturers whose build quality is highly impressive.

Screen or Stencil making however is the most crucial factor to get the best quality printing results. As they say, Screen printing is not a process it is an art, and so is the stencil making. Also, since PE coextruded tubes are printed in large quantities for a single artwork, the stencils or the mesh is generally not reclaimed. Thus, obtaining maximum impressions from a Screen is not only desirable, but also a challenge.
This article outlines post Screen making practices that screen makers can use to extend screen life and maximize the number of impressions. Because coextruded PE tubes are printed with UV inks, the guidance below applies specifically to that process.
Since you do not want to reuse the screens and are using strong UV inks, the best method is the Permanent Chemical Curing Process. This process changes the stencil into a hard plastic layer that will never wash off. It will easily handle thousands of prints without breaking down.
Step 1: Extra Light Cooking (Post-Exposure)
Before using chemicals, you need to make the stencil as hard as possible with light.
- Wash out your design and let the screen dry completely.
- Put the dry screen back into your UV exposure unit.
- Expose it inside for 4 to 5 times longer than your normal exposure time.
Step 2: Apply the Permanent Chemical (Hardener)
Use a heavy-duty permanent chemical hardener like ULANO or KIWI Screen hardener.
- Wet a sponge or soft cloth with the liquid hardener.
- Wipe a thin, even layer on both sides of the screen.
- Important: Take a clean, dry cloth and wipe away any extra liquid from the open areas of your design. If the chemical dries inside the holes, ink cannot pass through.
- Put the screen in a warm drying box or room heated to 40°C to 50°C. Let it bake at this temperature for 40 to 60 minutes.
Why this is the best method for UV Inks
- Strong Protection: UV inks have harsh chemicals that easily melt normal stencils. This process stops that completely.
- No Pinholes: It seals tiny weak spots, so you won’t get unwanted ink spots on your prints.
- Handles High Pressure: UV printing requires pressing hard against tough surface of PE tubes. The hard stencil processes as above will not rub off in such cases.
I have more than 35 years of experience in the screen-printing industry, including roles as plant head at several reputable organisations. At DR Optical Disc India Pvt Ltd., I also had a screen-making setup for over 15 years, where my team produced screens capable of more than 100,000 impressions. Even achieving 40,000–50,000 impressions per screen is commendable and cost-effective. Screens with shorter service lives increase manufacturing costs and cause production losses because stencils must be changed more frequently.
Recently, Ms. Vaaswee Sharma of Kaizen Manufacturing Pvt Ltd. along with Dhruva KS Rathore of DR Optical Disc https://cosmetictube.in/India Pvt. Ltd. discussed this issue with me in detail. As a renowned manufacturer of coextruded PE tubes, the company has achieved excellent print quality in a short time. Our discussion inspired me to write this blog and share my little knowledge of screen printing with others.
We at DR Optical Disc India Pvt. Ltd. have complete expertise in providing consultation for setting up a Cosmetic PE tube unit. This includes selection and sourcing of machinery, site preparation and layout, wiring & piping instructions, proper utilities selection and arranging trained manpower for the same. In fact, we have tie ups with some of the best equipment manufacturers across the globe for the PE tube manufacturing machinery. You can Call / WhatsApp Mr. Dhruva KS Rathore @ +91 9289091004 / 07, drop in a mail at director@droditech.com or explore our complete catalogue at https://cosmetictube.in/




Leave a comment